Encapsulation Manufacturing
Precision-fill capsule production from bench to commercial scale under 21 CFR Part 111 cGMP.
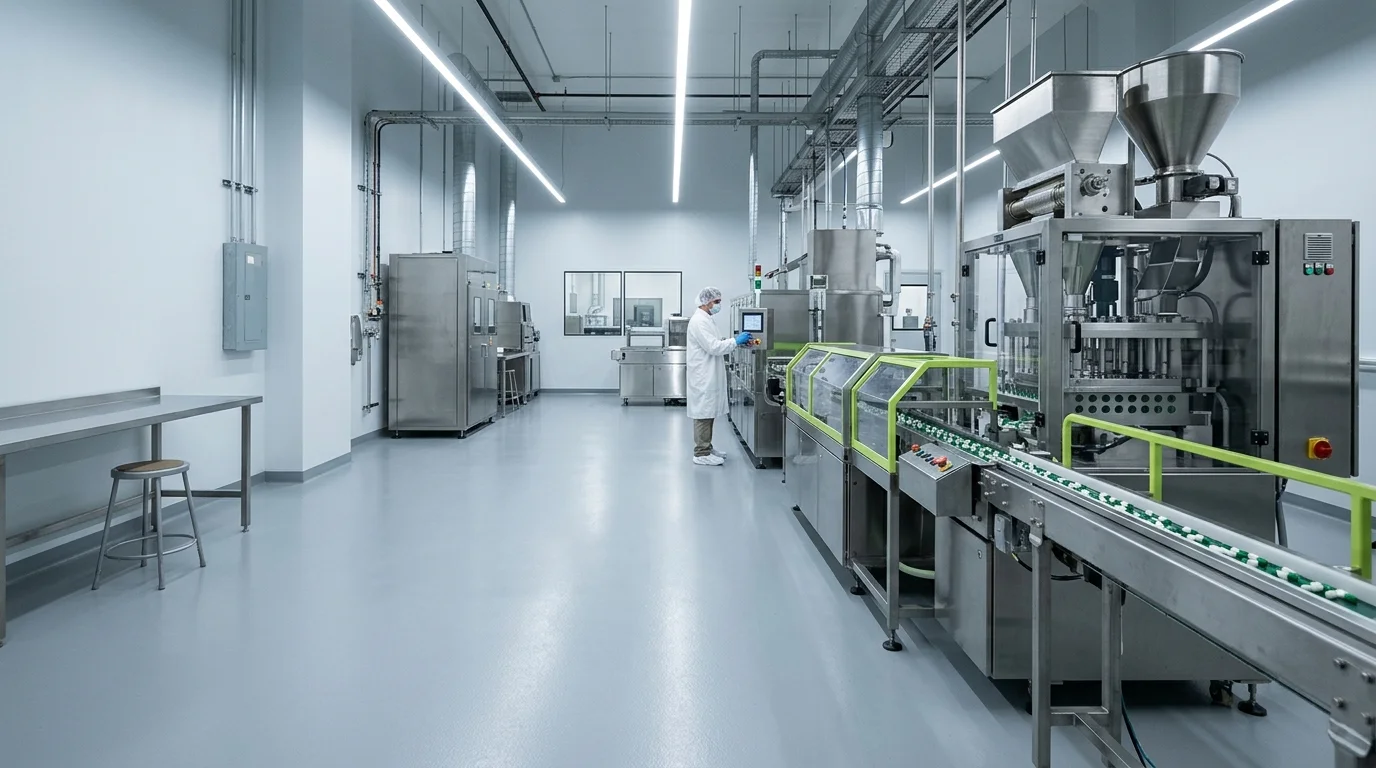
Our Carrollton and Van Alstyne facilities operate fully automated capsule filling lines capable of producing vegetarian HPMC, standard gelatin, delayed-release enteric, and beadlet-filled capsules. All encapsulation runs are governed by in-process weight uniformity checks every 15 minutes, with hard capsule disintegration confirmed per USP <701> before batch release.
Supported Dosage Forms & Formats
Quick Fact Sheet
Key production parameters
Minimum Order Quantity
1,000 finished units
Standard Lead Time
4–6 weeks from formula approval and PO
Cleanroom Standard
ISO Class 8 / 21 CFR Part 111 cGMP
Packaging Compatibility
- HDPE Bottles (60cc – 500cc, child-resistant caps)
- PET Amber Glass Bottles
- Blister Packaging (via partner)
- Bulk Drums (for resellers / repackagers)
- Stand-Up Pouches with zipper seal
- Clinical trial unit-dose sachets
Mutual NDA Standard: All formula details, BOM data, and brand concepts shared during the quoting process are protected under a reciprocal Non-Disclosure Agreement executed before technical evaluation begins.
Machinery & Specimen Visual Verification
Inspect actual cleanroom machinery, finished dosage macro specimens, and packaging protocols dedicated to encapsulation manufacturing.
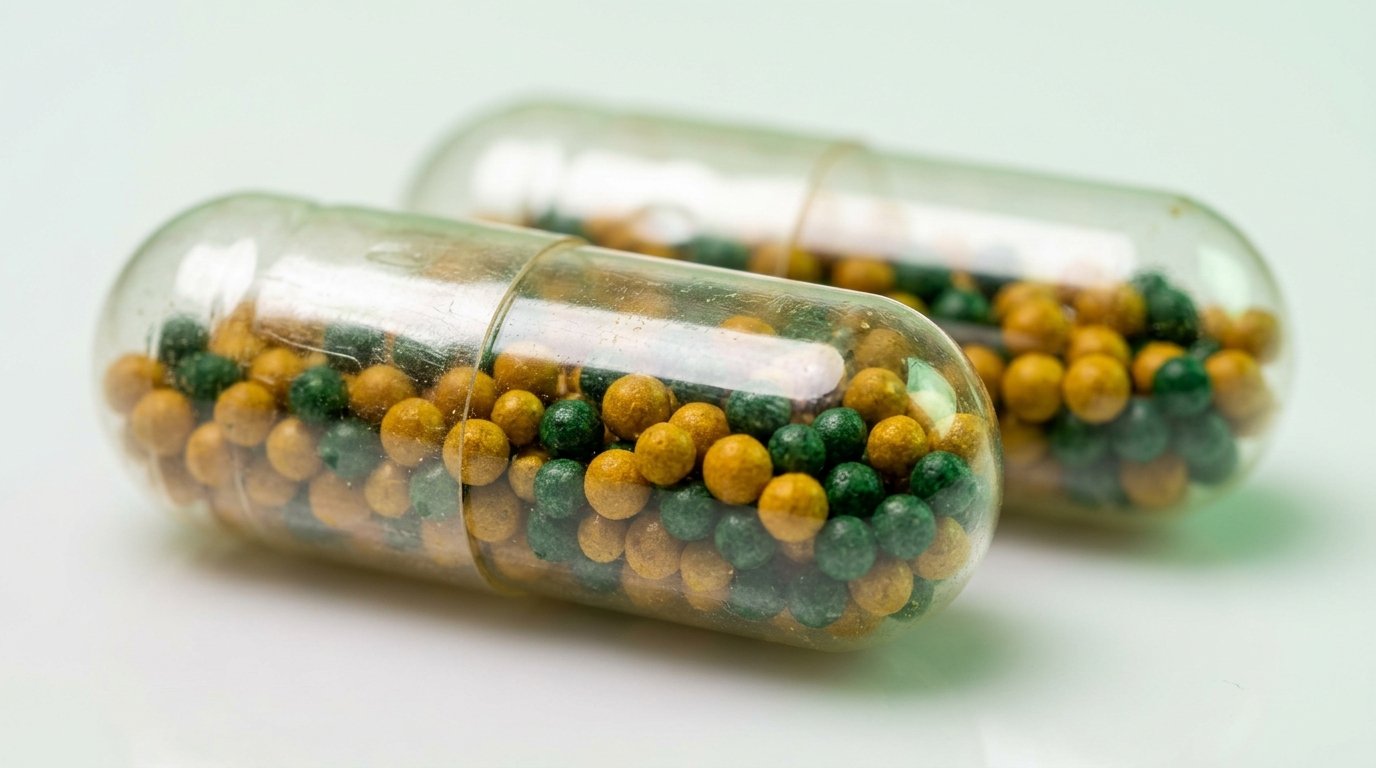
HPMC Vegetarian Two-Piece Capsules
Size 00 and 0 clear vegetarian capsules filled with standardized golden botanical extracts and delayed-release beadlets.

High-Speed Automated Rotary Encapsulation Line
Multi-tamping capsule filling machinery outputting up to 150,000 units/shift with continuous weight rejection.

Automated Bottling & Induction Foil Sealing
Integrated electronic counter, dessicant insert, induction seal, and automated bottle labeler.
Engineering Specification Table
Specifications are representative of standard production parameters. Project-specific values may vary based on formula requirements, ingredient characteristics, and target packaging format. Contact our engineering team for exact specifications relevant to your batch.
Quality Assurance & Verification Protocol
Every encapsulation manufacturing batch passes through a four-phase analytical verification workflow before Certificate of Analysis issuance and release.
Raw Material Identity & Purity
All active and excipient raw materials are identity-confirmed before release to production. COA cross-reference, organolpetic checks, and FTIR or HPLC assay performed based on ingredient risk classification.
In-Process Quality Monitoring
Continuous in-process controls during encapsulation: fill weight uniformity sampled every 15 minutes, visual capsule closure inspection, and real-time environmental monitoring of cleanroom temperature and RH.
Finished Product Testing
Complete finished-goods analytical release: potency assay against label claim, microbial enumeration (TPC, E. coli, Salmonella, Yeast & Mold), disintegration, and physical attribute confirmation.
Certificate of Analysis (COA) Release
QA Director review and sign-off of the complete batch record and analytical results. COA issued on MNL letterhead with full traceability to raw material lot numbers. No batch ships without COA authorization.
Certificate of Analysis (COA) — Issued Per Batch
Every commercial batch receives a QA Director–signed Certificate of Analysis on MNL letterhead. The COA documents all test parameters, analytical methods, results versus specification, and full lot traceability to raw material COAs. No batch ships without COA authorization.
Request a Quote for Encapsulation Manufacturing
Submit your project brief through our structured multi-step quote engine. Pre-select Encapsulation Manufacturing as your target manufacturing service. Our Carrollton, TX formulation and production team will provide a preliminary feasibility response within 24–48 business hours, under mutual NDA before any formula details are exchanged.
- Preliminary quote returned within 24–48 business hours
- Mutual NDA executed before formula review
- Direct access to MNL formulation chemists
Or contact our engineering team directly
(844)-323-5628info@micellecosmeticslabs.comMon – Fri: 8:00 AM – 5:00 PM CST. Facility visits by advance appointment.