Engineered for Purity.
Pharmaceutical-Grade Infrastructure.
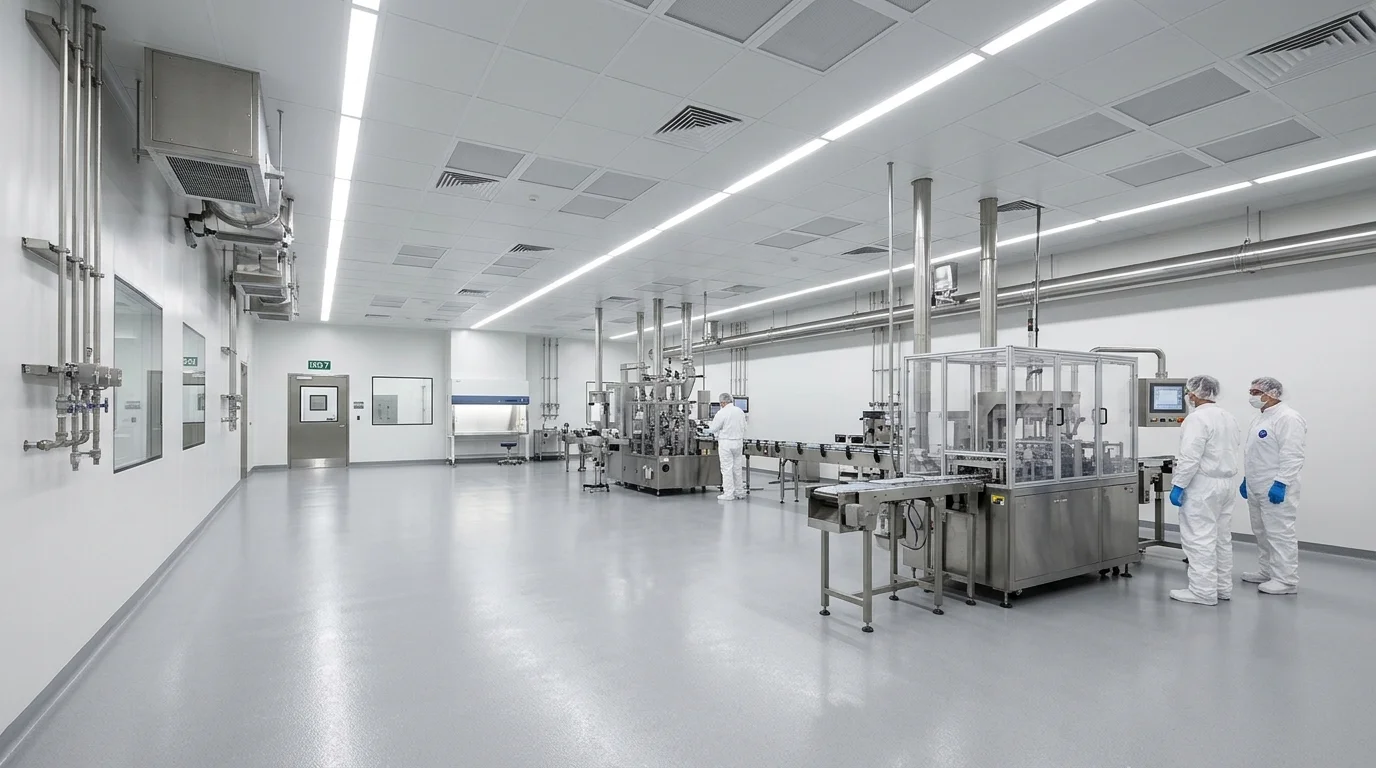
Dietary supplement manufacturing infrastructure operating under strict 21 CFR Part 111 cGMP standards across Carrollton and Van Alstyne, Texas. Featuring terminal HEPA cleanroom suites, tight relative humidity control (<20% RH), and automated rotary tableting and encapsulation lines.
Infrastructure Environmental Controls
Dietary supplements are sensitive to humidity, cross-contamination, and microbial intrusion. Our HVAC and clean utility architecture is modeled after modern pharmaceutical engineering standards.
HEPA Air Filtration & Air Changes
Terminal HEPA filtration captures 99.97% of airborne particulates down to 0.3 microns. Cleanroom suites maintain 20 to 30 air changes per hour (ACH) to ensure continuous dilution and evacuation of any ambient particulate matter.
Differential Pressure Cascades
Positive air pressure cascades (+15 to +25 Pascals) between processing suites and gowning airlocks ensure that air always flows outward, preventing external particulate entry into active open-product zones.
Desiccant Low-RH% Dehumidification
Specialized suites for effervescent drink powders and hygroscopic amino acids are equipped with industrial desiccant wheel dehumidifiers capable of holding relative humidity strictly below 20% to prevent clumping.
USP Purified Water & RO/DI Loop
Continuous multi-stage Reverse Osmosis (RO) with Electro-Deionization (CEDI) and UV loop sanitization producing purified water meeting USP monographs for liquid drops, tinctures, and sanitation CIP procedures.
Sanitary Epoxy & Coved Transitions
All production flooring is finished with seamless, chemical-resistant antimicrobial polyurethane epoxy with coved wall-to-floor junctions eliminating 90-degree corners where microbial bioburden or powder residue could harbor.
Continuous Environmental Monitoring
24/7 centralized Building Management System (BMS) logging temperature, humidity, pressure differentials, and dust particle counters with automated SMS/email alerts on any out-of-spec deviation.
Specialized Production Suites & Functional Zones
Segregated physical layouts to guarantee unidirectional flow of personnel and materials, preventing cross-contamination between botanicals, proteins, and active compounds.
Controlled RH% Cleanrooms & Production Suites
Engineered specifically for hygroscopic powders, botanical extracts, and effervescent formulations that degrade under atmospheric moisture.
- Desiccant dehumidifier units
- Digital magnehelic pressure gauges
- HEPA ceiling modules
- Gowning airlocks
High-Capacity Industrial Blending Suites
Precision micro-ingredient dispersion ensuring homogeneous coefficient of variation (<3% CV) even with active ingredients dosed as low as 50 mcg.
- V-Blenders (10 cu.ft. to 150 cu.ft.)
- Sanitary Ribbon Blenders (3,000L)
- Conical screw blenders
- Fluid-bed spray agglomerator
High-Speed Encapsulation & Tableting Core
High-efficiency solid dosage manufacturing equipped with real-time compaction force monitoring to guarantee tablet friability and dissolution.
- Automated Capsule Fillers (Size 00, 0, 1, 2, 4)
- Multi-station Rotary Tablet Presses
- Deduster & Metal Detector combos
- Weight checkweighers
Automated Packaging & High-Speed Bottling Lines
End-to-end automated secondary packaging delivering hermetically sealed, tamper-evident bottles, induction heat seals, and laser batch coding.
- Electronic multi-channel optical counters
- Automatic inline desiccant inserters
- Induction cap sealers
- Shrink wrap & pressure-sensitive labelers
In-House QA/QC Analytical & Wet Chemistry Lab
Equipped to handle raw material quarantine verification, real-time in-process checks, and final release COAs without relying solely on outside labs.
- HPLC / UPLC units
- ICP-MS trace metal analyzer
- FTIR spectrophotometer
- USP automated dissolution baths
- Microbiology incubators
Machinery & Daily Throughput Matrix
High-speed automated manufacturing lines engineered for tight operational tolerances, minimal changeover downtime, and continuous in-line quality verification.
| Machine Category | Model & Engineering Specs | Nominal Throughput | Operational Tolerances | Supported Formats | In-Line Quality Monitoring |
|---|---|---|---|---|---|
| Automated Capsule Filling | Rotary Multi-Tamping Pin Fillers | > 5,000,000 capsules / week | ±1.5% fill weight variance | Size 00, 0, 1, 2 (Gelatin, HPMC Vegetarian, Acid-Resistant) | 100% optical weight checkweighing & electronic capsule height sorting |
| High-Speed Rotary Tableting | 36-Station Double-Sided Rotary Tablet Presses | Up to 150,000 tablets / hour | Friability < 0.5%, Hardness 4 - 18 kp | Round, Oval, Oblong, Chewables, Bi-layer, Sublinguals | Automatic rejection gate based on punch-compression force deviation |
| Sanitary Powder Blending | Sanitary 316L Stainless Steel V-Blenders & Ribbon Blenders | 25,000 lbs (11,300 kg) / day | Coefficient of Variation (CV) < 3.0% | Plant & Whey Protein, Hydration Electrolytes, Nootropics, Pre-workouts | 10-point core thief sampling across blender vessel prior to discharge |
| Automated Bottling Line | Multi-Head Optical Counting & Inline Capping System | 60 - 90 bottles / minute | 100% count accuracy with dual infra-red beams | 60cc to 950cc PET & HDPE bottles, glass amber jars | Enercon induction seal integrity verification & vision inspection |
| Multi-Lane Stick Pack & Sachet Packaging | Vertical Form-Fill-Seal (VFFS) High-Speed Machinery | Up to 120 sachets / minute | ±0.05g fill weight accuracy | Single-serve drink mixes (2g - 25g), Gusset foil pouches | Continuous nitrogen flushing with residual O2 monitoring (<2%) |
| Liquid Tincture & Dropper Filling | Piston & Peristaltic Cleanroom Liquid Fillers | 3,000 bottles / hour | ±0.2 ml volumetric dosage accuracy | 15ml, 30ml, 60ml, 120ml glass tincture bottles with graduated pipettes | In-line torque monitoring for tamper-evident closures |
Inside Our Texas Manufacturing Core
Step through our Carrollton and Van Alstyne facilities. Explore five critical manufacturing stages engineered to meet strict 21 CFR Part 111 standards.


ISO Class 7 cGMP Primary Cleanroom Suite
Positive pressure (+20 Pa) suites equipped with terminal HEPA filtration (0.3 micron at 99.97% efficiency) eliminating ambient airborne particulates.
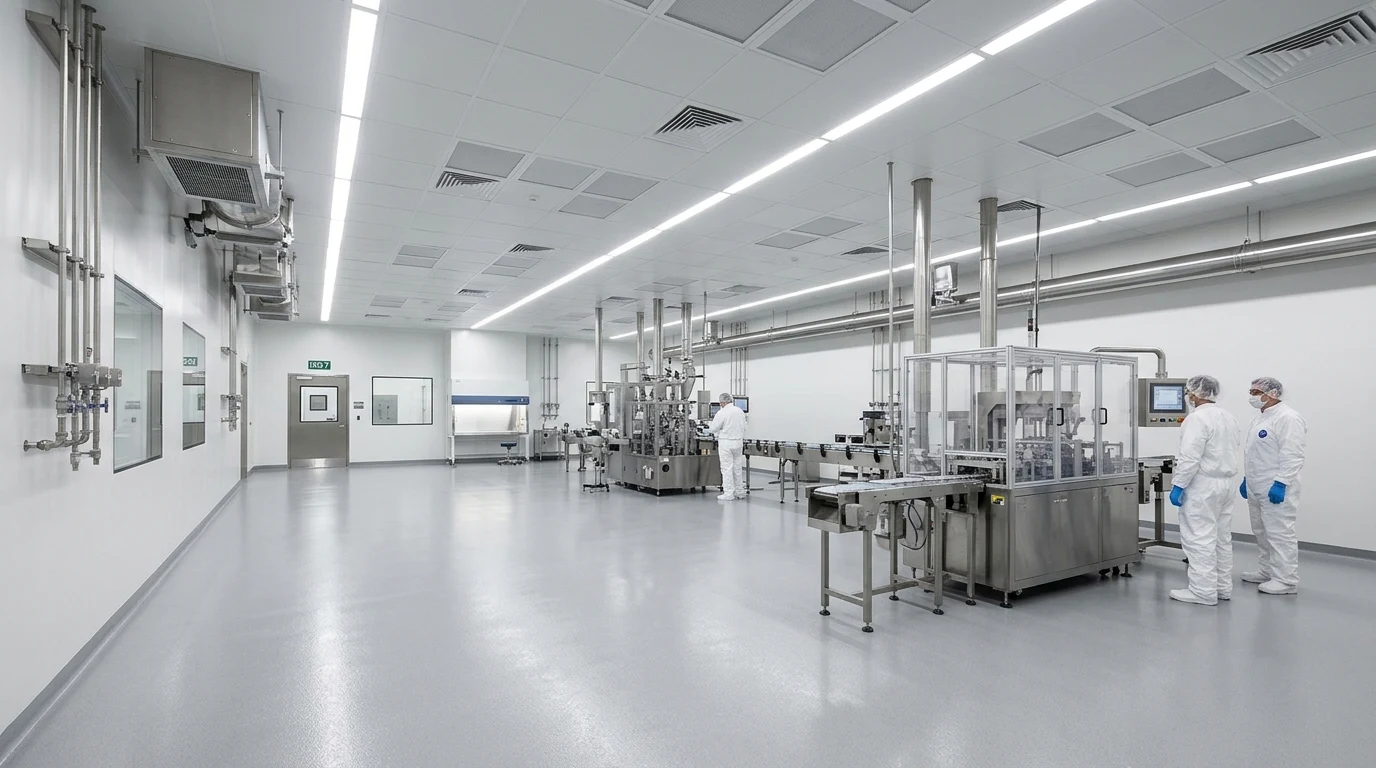
Analytical QA & Cleanroom Encapsulation Center
Location: 4717 Plano Parkway Suite #150, Carrollton, TX 75010. Houses our in-house HPLC/ICP-MS analytical testing laboratory, cleanroom capsule/tablet manufacturing lines, and executive client formulation suites.
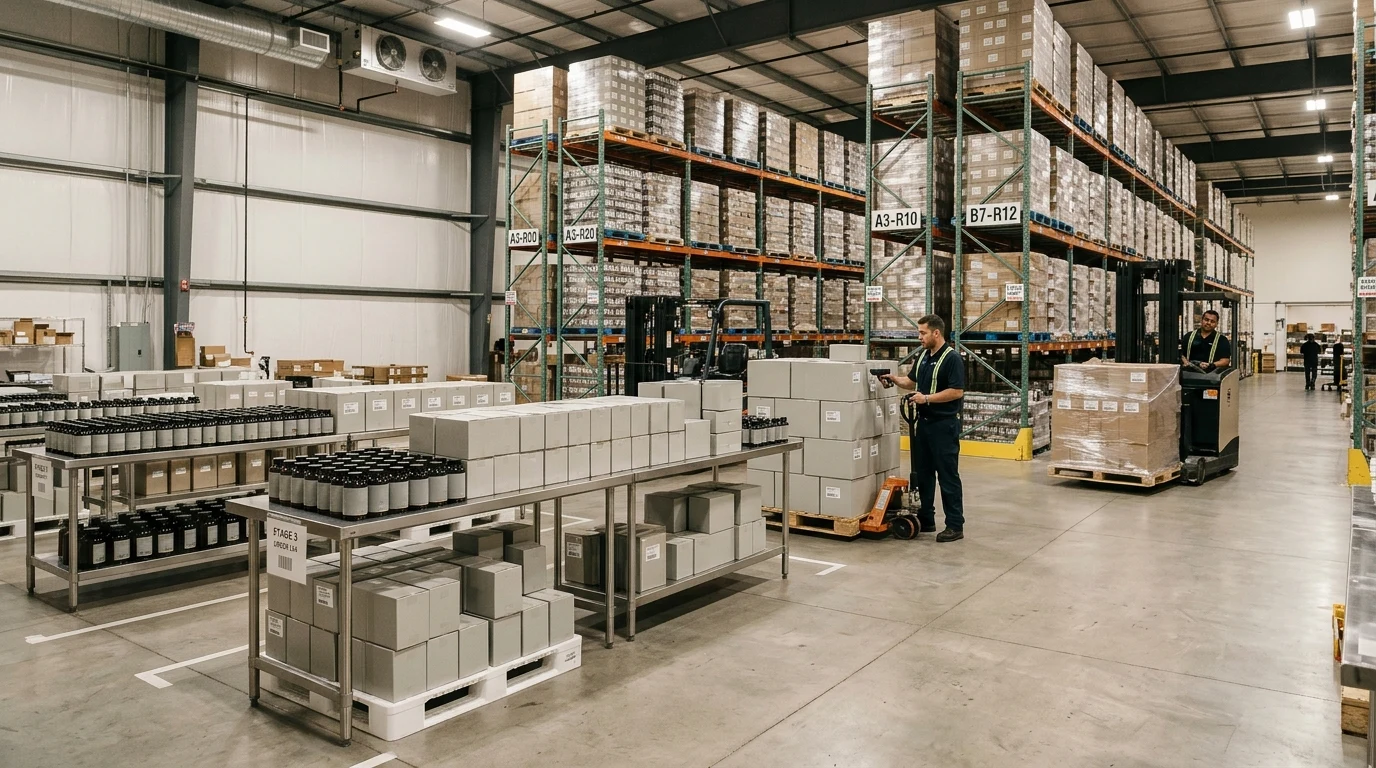
Bulk Powder Blending & High-Speed Bottling Hub
Location: Van Alstyne, TX. Our high-capacity industrial production campus featuring 25,000 lbs/day blending capacity, automated high-speed bottling conveyors, and 65,000 sq. ft. of climate-controlled warehousing.
Verify Our Capabilities Firsthand
Experience our cleanroom disciplines, environmental controls, and automated throughput in person. Speak directly with our Chief Formulator and VP of Quality in Carrollton, Texas.