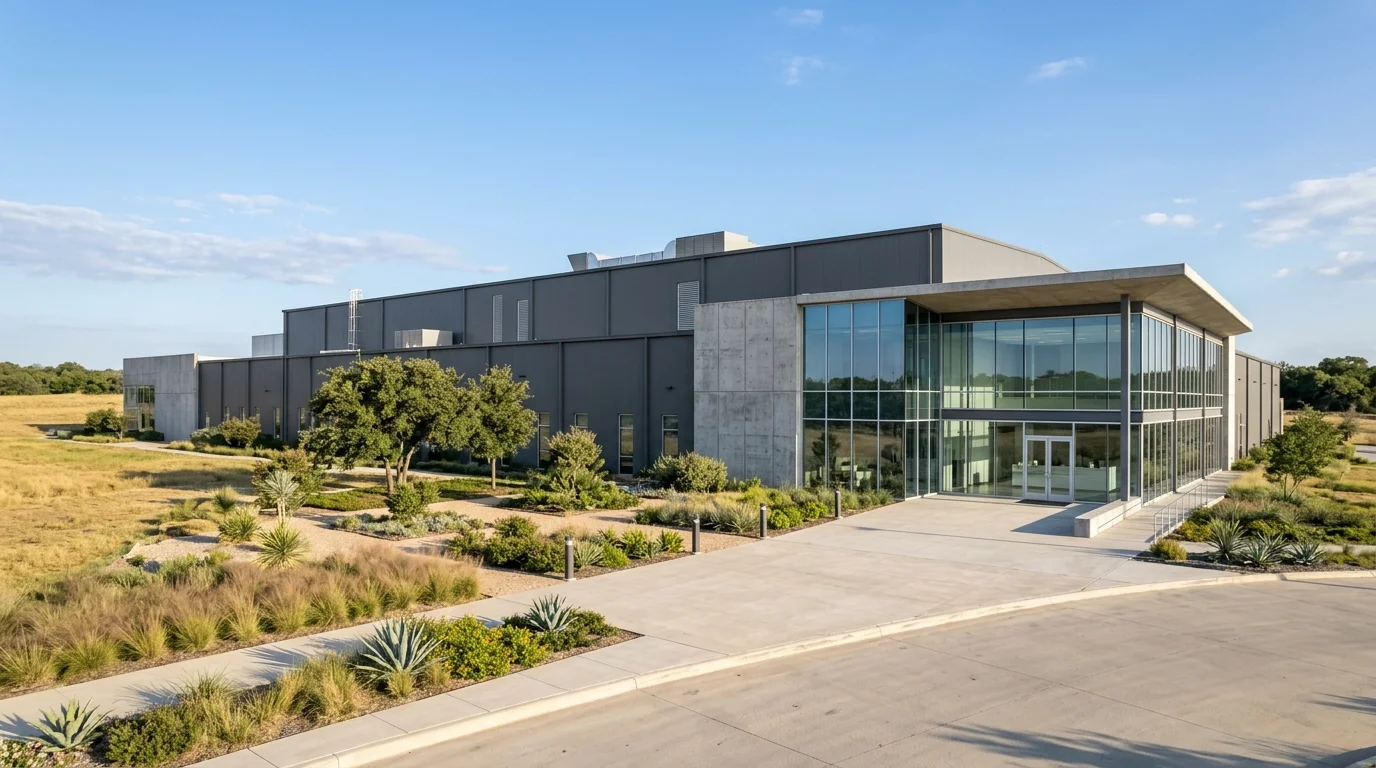
Pharmaceutical Rigor.
Nutraceutical Innovation.
Founded by formulation chemists and manufacturing engineers in Texas, Micelle Nutraceuticals Labs was established to solve contract manufacturing's greatest pain points: opaque analytical data, unpredictable lead times, and excipient compromises. We operate as an authentic, science-first partner for brands that refuse to compromise on label integrity.
Bridging the Gulf Between Research Labs and High-Volume Retail Shelves
Micelle Nutraceuticals Labs was founded in Dallas-Fort Worth by a group of pharmaceutical chemists and nutrition scientists who witnessed a systemic flaw in supplement manufacturing: contract manufacturing had become a commodity business dominated by cut corners, unaccountable lead times, and underdosed formulas hidden behind proprietary blends.
We built MNL on the conviction that dietary supplement manufacturing must meet the same analytical discipline as pharmaceutical production. Today, operating across our Carrollton analytical center and Van Alstyne production campus, we provide full turnkey CDMO services designed specifically for brands that refuse to compromise.
“To serve as the definitive catalyst that transforms groundbreaking nutritional research into compliant, market-defining products on retail shelves.”
We stand as an unyielding technical bridge between clinical nutrition research and commercial scale. Through rigorous analytical release, modern delivery technologies, and absolute non-disclosure protection for proprietary intellectual property, we empower brands to scale confidently.
150,000+ Sq. Ft Texas Operations & Scientific Leadership
Our dual-campus Texas presence combines precision ISO 7 encapsulation cleanrooms, high-capacity commercial powder blending, and in-house analytical chemists.
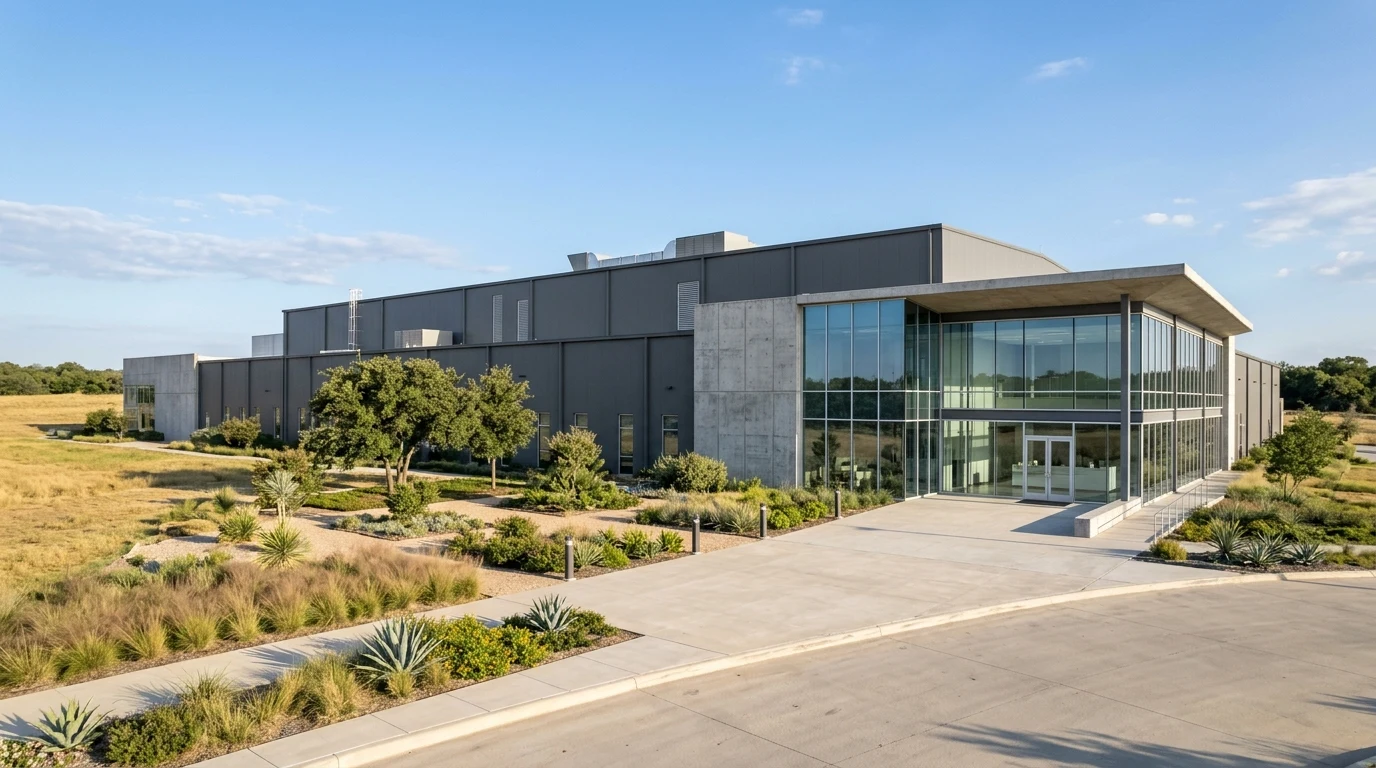
Carrollton Analytical & Encapsulation Campus
Class 10,000 cleanroom suites operating automated capsule fillers, rotary tablet presses, and positive-pressure climate controls with complete electronic batch records.
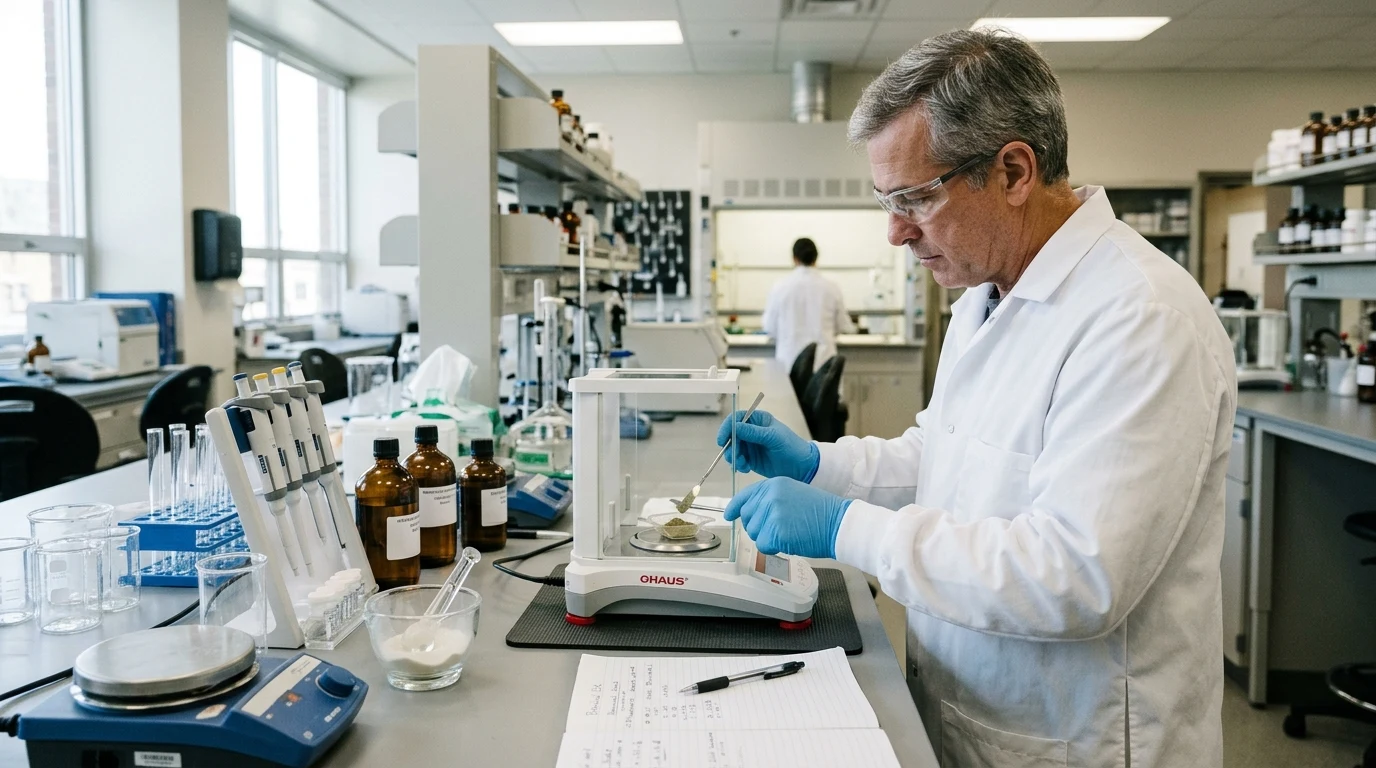
Scientific R&D & Analytical Formulation Core
Our internal laboratory leaders, degreed analytical chemists, and food scientists engineer bioavailability curves, stability profiles, and custom taste-masking technologies.
Three Non-Negotiable Core Values
Every decision on our cleanroom floors, every supplier partnership, and every batch release is governed by these foundational principles.
Absolute Transparency
We believe trust is forged through open data. Every client receives unrestricted visibility into lot-specific Certificates of Analysis (COA), Master Manufacturing Records (MMRs), and exact test metrics. No hidden proprietary blends, no artificial padding, and no obfuscation.
Scientific Innovation
Formulation is an exact biochemical science, not mere ingredient mixing. We pioneer advanced delivery technologies, micro-encapsulation, natural taste masking, and bioavailability optimization that transform complex actives into highly marketable consumer products.
Zero Tolerance for Substandard Ingredients
A supplement is only as safe as its weakest raw input. We enforce mandatory FTIR identity screening on 100% of incoming lots and trace ICP-MS heavy metal verification. Contaminated, adulterated, or under-strength lots are rejected back to the supplier instantly.
Multidisciplinary Scientific & Production Team
We don't just operate machines. Our teams include degreed analytical chemists, food scientists, and regulatory affairs specialists working collaboratively on every project.
Executive Leadership & Operations
Strategic capacity scaling, capital equipment investment, and strict 21 CFR Part 111 cGMP compliance oversight across Carrollton and Van Alstyne facilities.
Formulation & Sensory Science
Bioavailability matrix optimization, natural organic flavoring, chewable tablet texture engineering, and rapid pilot bench testing.
Analytical QA/QC Laboratory
HPLC active potency assay, ICP-MS trace elemental detection, USP disintegration testing, and independent lot release authorization.
Cleanroom Production & Engineering
Automated high-speed encapsulation, high-capacity sanitary powder blending, and positive-pressure cleanroom environmental management.
Milestones of Growth & Capability Expansion
From our Dallas roots to our current dual-campus Texas infrastructure, every year has been marked by strategic investments in analytical equipment and cleanroom capacity.
Inception in Dallas, Texas
Founded by pharmaceutical formulation specialists in the Dallas-Fort Worth area, initially innovating advanced topical and emulsion delivery systems.
FDA Dietary Supplement Registration
Formally registered facility with the FDA CFSAN, establishing our 21 CFR Part 111 cGMP compliance framework for solid and liquid oral supplements.
Van Alstyne Bulk Blending Expansion
Inaugurated our second Texas campus in Van Alstyne to house 25,000 lbs/day powder blending capacity and high-speed automated bottling lines.
In-House Analytical Laboratory Upgrade
Commissioned internal HPLC and ICP-MS testing suites at Carrollton, slashing lot release turnaround from weeks down to 5–7 business days.
Clean Label & NSF for Sport Alignment
Expanded cleanroom suites to meet strict WADA and professional athletic banned substance screening requirements for top-tier sports nutrition brands.
Next-Generation CDMO Platform
Serving hundreds of domestic and international dietary brands with end-to-end turnkey development, real-time batch traceability, and rapid lead times.
Partner With a Manufacturing Team That Prioritizes Your Science
Speak directly with our Texas R&D team about custom formulation development, contract manufacturing, or transferring an existing commercial product line.