cGMP Facility • Texas
Carrollton & Van Alstyne, Texas

Comprehensive CDMO Contract Manufacturing Capabilities

From bench-scale R&D in our Carrollton formulation lab to high-volume commercial blending, encapsulation, and liquid filling at our Van Alstyne manufacturing campus — MNL delivers end-to-end supplement manufacturing under a single, FDA-registered, cGMP-compliant roof.

Showing 12 of 12 manufacturing capabilities
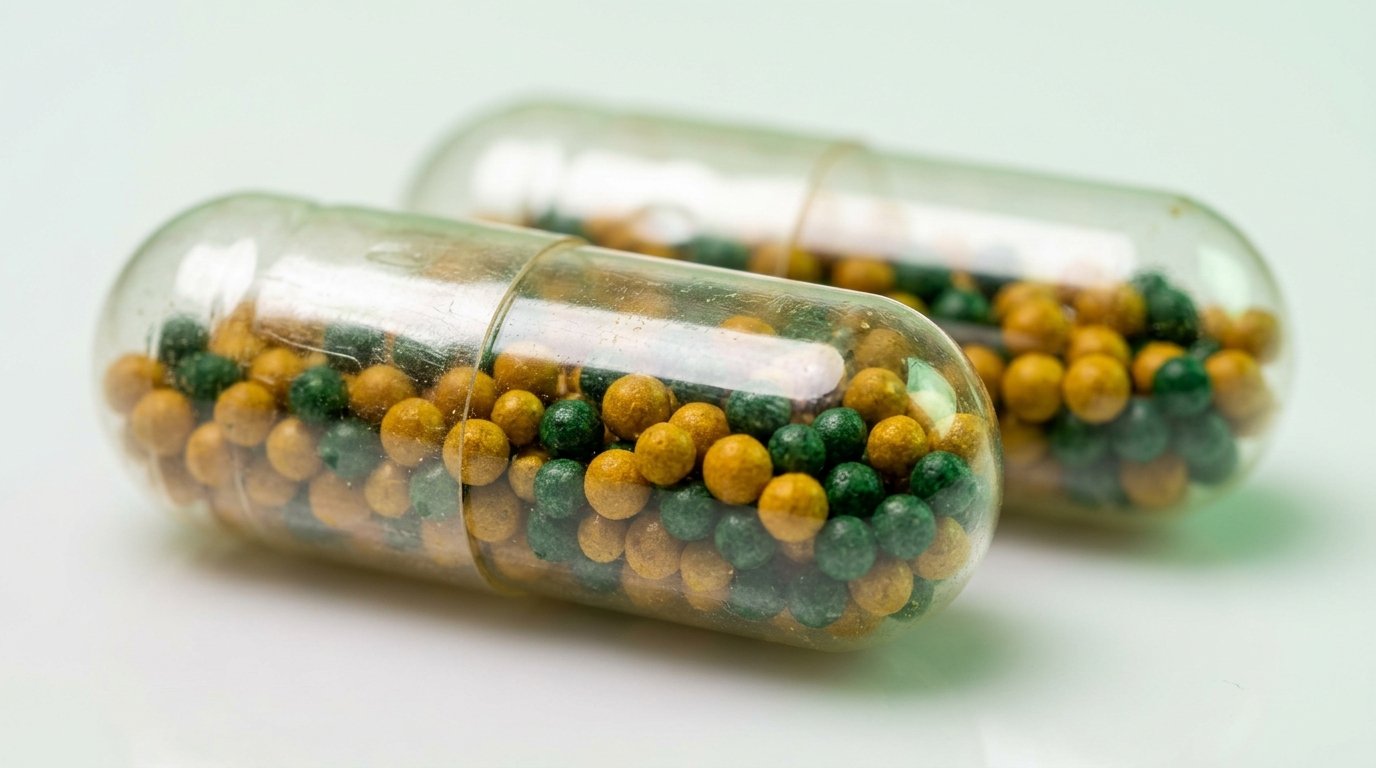
Two-piece vegetarian HPMC capsules filled with standardized golden botanicals
Supplements Manufacturing150K Caps / 8h Shift
ISO Class 8 / 21 CFR Part 111 cGMPMOQ: 1,000 finished units

Encapsulation Manufacturing

Precision-fill capsule production from bench to commercial scale under 21 CFR Part 111 cGMP.
Minimum Order Quantity (MOQ)1,000 units
Standard Commercial Run5,000 – 100,000+ units per batch
Line Speed (automated)Up to 150,000 capsules / 8-hour shift
View Engineering Specifications
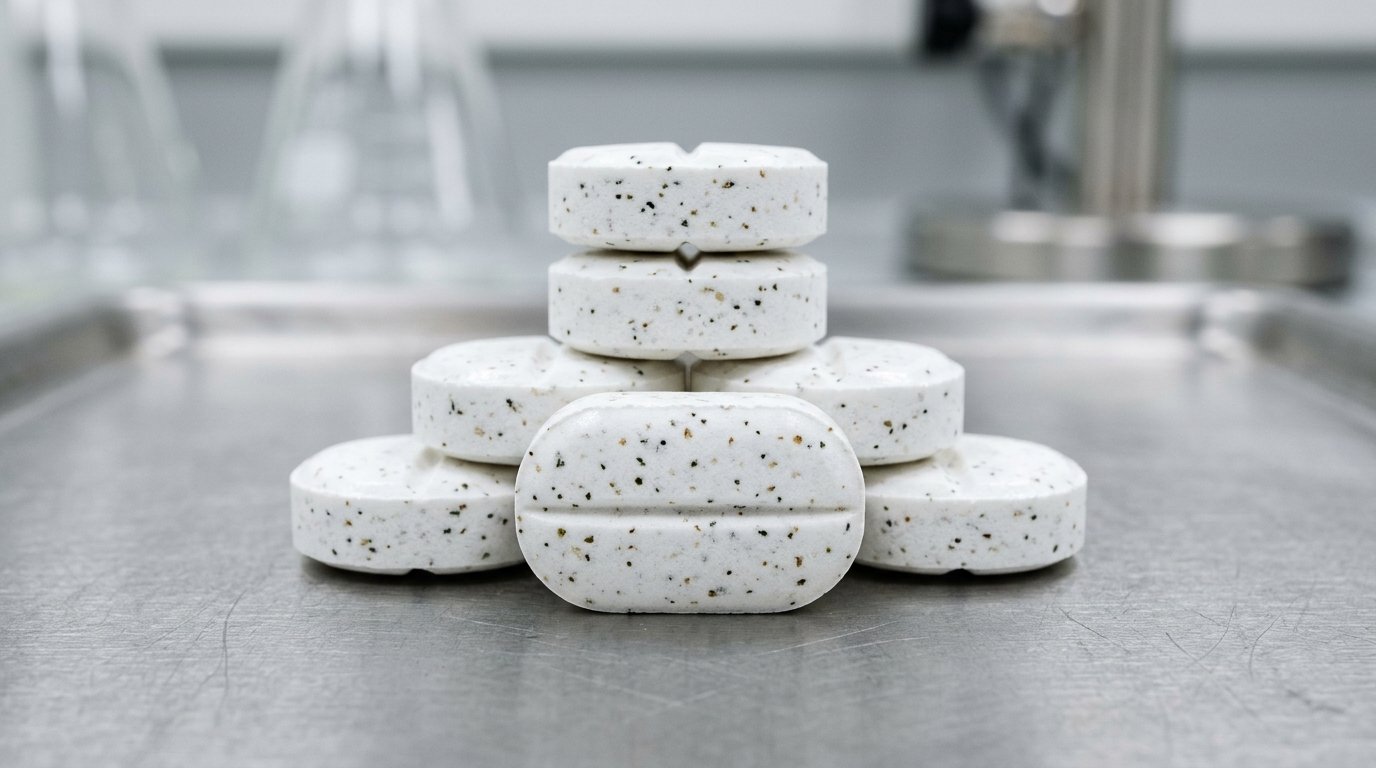
Precision-pressed scored pharmaceutical white tablets
Supplements ManufacturingRotary Compression
ISO Class 8 / 21 CFR Part 111 cGMPMOQ: 2,000 finished units

Tablet Manufacturing & Rotary Compression

Film-coated, chewable, bi-layer, and sublingual tablet production on high-speed rotary presses.
Minimum Order Quantity (MOQ)2,000 units
Tablet Press TypeMulti-station rotary press (direct compression + wet granulation)
Tablet Hardness Range4 – 20 kP (configurable per formulation)
View Engineering Specifications
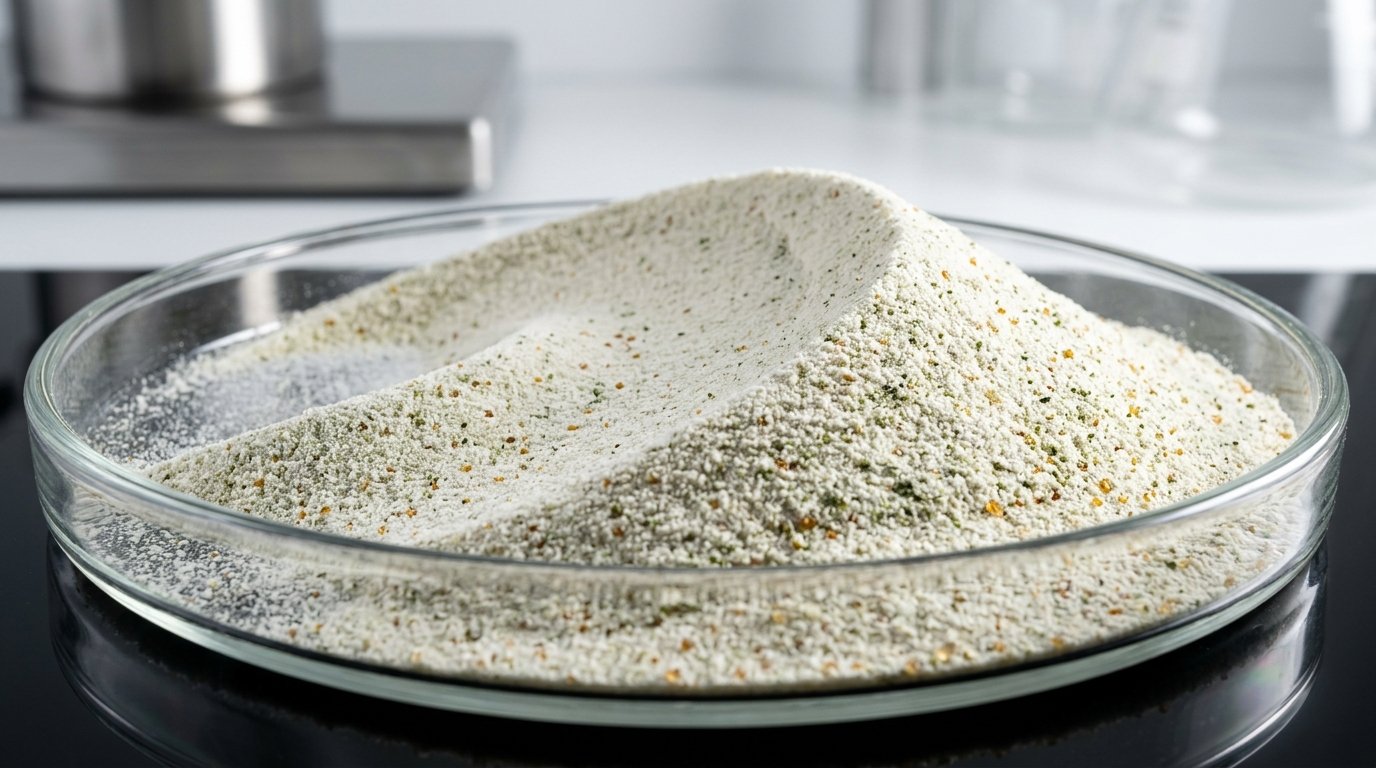
Fluid-bed agglomerated electrolyte and superfood powder
Supplements ManufacturingInstantized Agglomeration
Controlled environment / 21 CFR Part 111 cGMPMOQ: 1,000 units (retail) / 100 kg (bulk)

Powder Manufacturing & Industrial Blending

High-shear blending, instantization, and agglomeration for sports nutrition, wellness, and clinical powder formats.

Pilot Batch Size25 – 100 kg
Commercial Batch Size100 – 2,000 kg per batch
Blender TypesRibbon, V-blender, High-shear granulator, Bin blender
View Engineering Specifications
Amber glass sublingual dropper bottle with pure golden tincture droplet
Supplements ManufacturingNano-Emulsion Carrier
ISO Class 8 liquid filling suite / 21 CFR Part 111 cGMPMOQ: 500 units

Liquid Manufacturing & Tinctures

Aqueous, oil-based, and nano-emulsified liquid supplement manufacturing with aseptic-grade filling.

Minimum Batch Size50 liters (pilot); 500 liters (commercial)
pH Control RangepH 3.0 – 8.5 (aqueous formulas)
Nano-emulsion Particle Size< 200 nm (D90) by dynamic light scattering
View Engineering Specifications
Sanitary 316L powder blending suite for whey protein isolate and plant proteins
Supplements Manufacturing25,000 lbs/Day Bulk
Controlled environment / 21 CFR Part 111 cGMPMOQ: 500 kg (bulk) / 1,000 retail units

Protein Manufacturing (Plant & Dairy)

Precision protein blend manufacturing across pea, rice, whey, and casein matrices for sports and wellness brands.
Protein Source Purity (whey isolate)≥ 90% protein by dry weight
Protein Source Purity (pea isolate)≥ 80% protein by dry weight
Nitrogen Test MethodKjeldahl / Dumas combustion method per AOAC
View Engineering Specifications
Sports nutrition pre-workout and hydration powder matrix blending in Texas cleanroom
Supplements ManufacturingWADA Compliant
Controlled environment / 21 CFR Part 111 cGMP; NSF for Sport® readyMOQ: 1,000 retail units

Sports Nutrition & Performance Formulas

Pre-workout, intra-workout, and recovery formula manufacturing for athletic and performance supplement brands.

Active Ingredient Count per SKUUp to 25 actives per blend formula
Stimulant SystemsCaffeine anhydrous, Dicaffeine malate, TeaCrine® (license req.)
Creatine Purity StandardCreatine monohydrate ≥ 99.9% purity by HPLC
View Engineering Specifications
Low-humidity temperature-controlled live strain probiotic encapsulation
Supplements ManufacturingDRcaps Moisture Lock
ISO Class 8 / 21 CFR Part 111 cGMP; dedicated probiotic fill roomMOQ: 1,000 finished units

Probiotics & Microbiome Manufacturing

Lyophilized probiotic blend manufacturing with guaranteed CFU viability at time of expiry.
CFU Overage StrategyMinimum 20% overage above label at time of manufacture to ensure viability at expiry
Strain Count RangeSingle-strain to 15-strain custom blend
CFU Range (label)1 billion – 100 billion CFU per serving
View Engineering Specifications
Chelated mineral and multivitamin tablet manufacturing
Supplements ManufacturingUSP Disintegration
ISO Class 8 / 21 CFR Part 111 cGMPMOQ: 2,000 finished units

Vitamin & Mineral Complex Manufacturing

Precision micronutrient dosing for multivitamin, mineral, and targeted supplement SKUs at commercial scale.
Vitamin Source OptionsUSP-grade vitamins; methylated B12 (methylcobalamin) & folate (5-MTHF) available
Mineral Form OptionsAlbion® TRAACS chelates, citrates, gluconates, oxides
Fat-Soluble Vitamin HandlingVitamins A, D3, E, K2 in oil-dispersion or encapsulated beadlet form
View Engineering Specifications
High-potency strength formulation and active capsule fills
Supplements Manufacturing100% Active Assay
Controlled environment / 21 CFR Part 111 cGMPMOQ: 1,000 units

Bodybuilding & High-Performance Formulas

Mass gainer, thermogenic, and hormone-support supplement manufacturing for physique and strength athletes.
Caloric Density (mass gainers)300 – 1,200+ kcal per serving (formulation-specific)
Herbal Extract StandardizationKSM-66® Ashwagandha (5% withanolides), Tongkat Ali (1:200 extract)
Thermogenic Ingredient RangeCaffeine anhydrous, green tea extract (EGCG), cayenne pepper extract
View Engineering Specifications
Sensory analytical flavor laboratory and natural taste-masking development
R&D & Value-Added ServicesNatural Taste Masking
R&D flavor lab / 21 CFR Part 111 compliant scale-upMOQ: R&D service — no unit MOQ; batch production MOQ applies at scale-up

Flavor Development & Natural Taste Masking

Custom flavor engineering and bitter masking for nutraceutical powders, liquids, and oral solid dose forms.

Flavor System TypesNatural flavors (FTNF), natural & artificial (N&A), artificial flavors
Bitter Masking AgentsCyclodextrins, ion exchange resins, spray-dried encapsulation, masking flavor compounds
Sweetener SystemsSucralose, stevia (Reb-A, Reb-M), monk fruit, erythritol, acesulfame-K
View Engineering Specifications
316L mirror-polished sanitary industrial V-blender suite
R&D & Value-Added ServicesRSD < 3.0% Uniformity
R&D lab + 21 CFR Part 111 compliant production scale-upMOQ: R&D service — formulation fees apply; production MOQ applies at scale-up

Custom Blending & Formulation Services

Contract blending and private-label formulation from concept brief to production-ready master formula.
Formulation ScopeAll dietary supplement categories under DSHEA 1994
R&D Pilot Batch Size1 – 10 kg bench; 25 – 100 kg pilot blender
Stability ProtocolAccelerated (40°C/75% RH) and real-time (25°C/60% RH) available
View Engineering Specifications
Automated multi-head packaging and turnkey fulfillment logistics
Packaging & Fulfillment80-120 Bottles/Min
Climate-controlled logistics facility / 21 CFR Part 111 cGMP warehouse protocolsMOQ: 1 pallet (warehousing); 500 units (label application); 250 kits (kit assembly)

Printing, Kitting & Nationwide Fulfillment

Complete post-manufacturing logistics: labeling, kitting, warehousing, and nationwide distribution from Carrollton, TX.

Label Compliance Review21 CFR Part 101 dietary supplement labeling compliance audit included
Label PrintingDigital and flexographic, full-color, primary and secondary labels
Label Application SpeedUp to 3,600 units/hour (automated label applicator)
View Engineering Specifications

21 CFR Part 111 cGMP

Every batch produced at MNL adheres to FDA dietary supplement current Good Manufacturing Practices. No exceptions.

In-House QC Testing

Our on-site laboratory performs identity, potency, microbial, and physical testing before any batch is authorized for release.

Mutual NDA Standard

All proprietary formulas and brand data are protected under a reciprocal Mutual NDA executed before any technical discussion begins.

Technical Formulation & Manufacturing

Ready to specify your manufacturing run?

Select a service above to review full technical specifications, then submit your project brief through our multi-step quote engine for a preliminary feasibility response within 24–48 hours.

Start Quote Engine